Tel/WhatsApp
0086-135 2669 2320

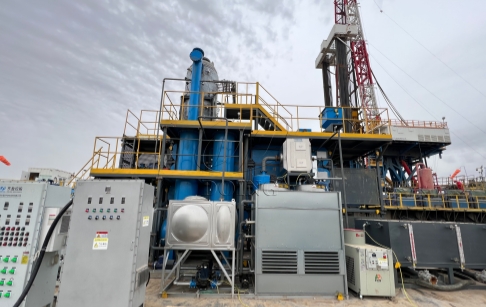
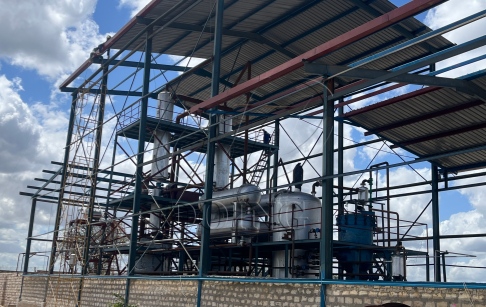
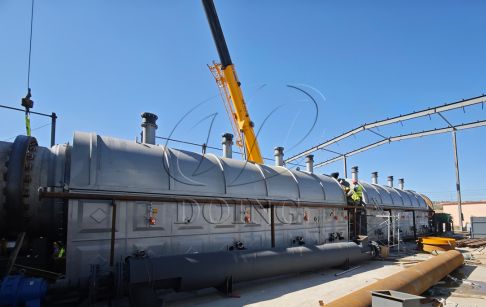
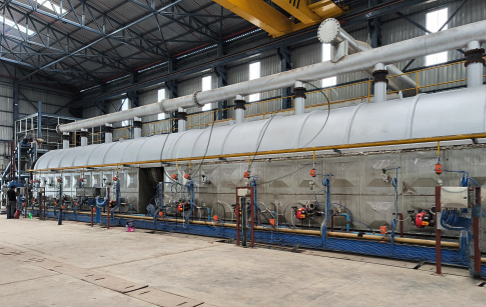
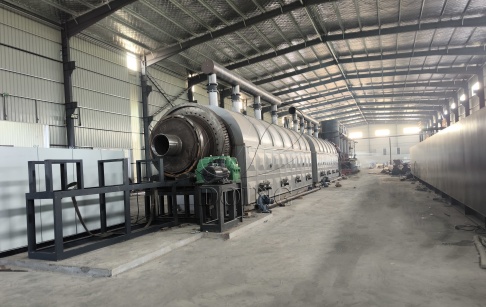
In September 2026, a customer confirmed an order with DOING ECO for two 15TPD tire pyrolysis plants and 15TPD oil refining and purification capacity for a waste tire recycling project in Mombasa, Kenya.
The two pyrolysis plants will provide a combined waste tire processing capacity of 30 TPD, while the downstream refining and purification system has a capacity of 15 TPD. The equipment is now entering production and will be shipped to Kenya after manufacturing is completed.
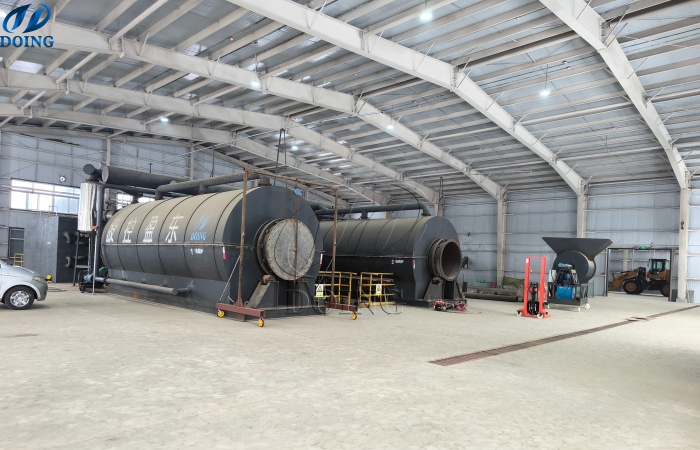 Waste tire pyrolysis recycling to fuel project Kenya
The project is based on two individual 15TPD tire pyrolysis units rather than one 30TPD unit.
| Item | Project configuration |
| Tire pyrolysis equipment | 15 TPD × 2 |
| Combined tire processing capacity | 30 TPD |
| Oil refining and purification | 15 TPD |
| Project location | Mombasa, Kenya |
| Process route | Waste tires → pyrolysis oil → refining & purification → refined oil |
With two 15TPD plants operating together, the project has a combined processing capacity of 30 tons of waste tires per day.
Using 330 operating days per year as a planning reference:
30 TPD × 330 days = approximately 9,900 tons of waste tires per year
This gives the project an annual waste tire processing scale of around 9,900 tons, although actual throughput will depend on operating days, maintenance periods, feedstock availability and operating conditions.
For a project of this size, the annual waste tire supply should therefore be considered alongside the equipment capacity when planning the site and logistics.
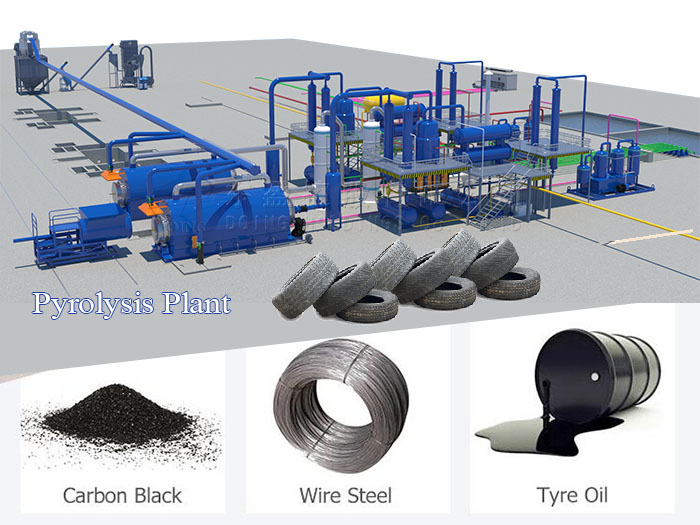 Products of waste tire pyrolysis
The pyrolysis stage converts waste tires into pyrolysis oil, recovered carbon black, steel wire and non-condensable gas.
Using a reference pyrolysis oil yield of 40–45%, processing approximately 9,900 tons of waste tires per year could result in an estimated:
| Reference | Estimated pyrolysis oil |
| Annual waste tire input | ~9,900 tons |
| At 40% oil yield | ~3,960 tons/year |
| At 45% oil yield | ~4,455 tons/year |
These figures are estimated pyrolysis oil output before downstream refining and purification. They should not be treated as the final annual volume of refined fuel, because the refining stage has its own process losses and product specifications.
The project therefore combines two separate capacity considerations: the 30 TPD combined tire pyrolysis capacity and the 15 TPD oil refining and purification capacity.
The project process can be understood in two main stages:
Stage 1 — Tire pyrolysis
Two 15TPD tire pyrolysis plants process prepared waste tires and recover pyrolysis oil together with recovered carbon black, steel wire and non-condensable gas.
Stage 2 — Oil refining and purification
Part of the pyrolysis oil is then processed through the 15TPD refining and purification system to improve its quality for the customer’s intended application.
The customer’s technical discussions focused particularly on the application of the refined oil, including whether it could be used as fuel for generators. This was an important consideration during the equipment evaluation before the order was confirmed.
 Waste tire pyrolysis equipment for producing non-standard diesel fuel
The customer first visited DOING ECO for technical discussions on May 12, 2026.
During the project evaluation, the customer reviewed the tire pyrolysis process, equipment configuration and downstream oil treatment requirements. The application of the refined oil was also discussed, particularly its potential use in generator fuel applications.
A second visit took place on September 2, 2026, with the investor participating in the technical discussion and reviewing the project in greater detail.
The customer had also considered other suppliers during the evaluation process. According to the project discussions, factors including timely technical responses, communication on the process requirements and the manufacturer’s production capability contributed to the final equipment selection.
After the technical discussion on September 2, the customer completed payment and the order was confirmed.
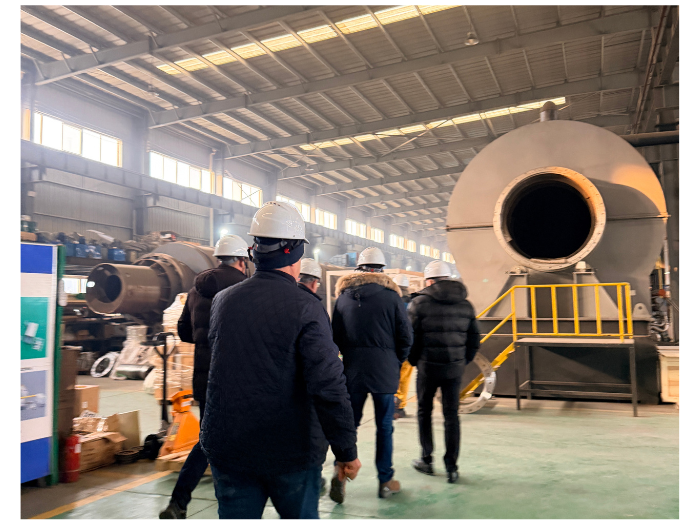 Client visits the waste tire pyrolysis project site
The confirmed order includes:
2 × 15TPD tire pyrolysis plants
15TPD oil refining and purification capacity
30 TPD combined waste tire processing capacity
Based on 330 operating days, the two pyrolysis plants could process approximately 9,900 tons of waste tires per year. At a reference oil yield of 40–45%, the annual pyrolysis oil output could be around 3,960–4,455 tons before refining.
The equipment is now entering production at DOING ECO. After manufacturing and inspection are completed, the equipment will be shipped to the customer’s project site in Mombasa, Kenya.
For waste tire recycling projects, equipment capacity, annual feedstock availability, pyrolysis oil recovery and downstream refining capacity need to be evaluated together. DOING ECO can provide project-specific equipment configurations based on the required tire processing capacity and oil treatment requirements.